Scotland-based
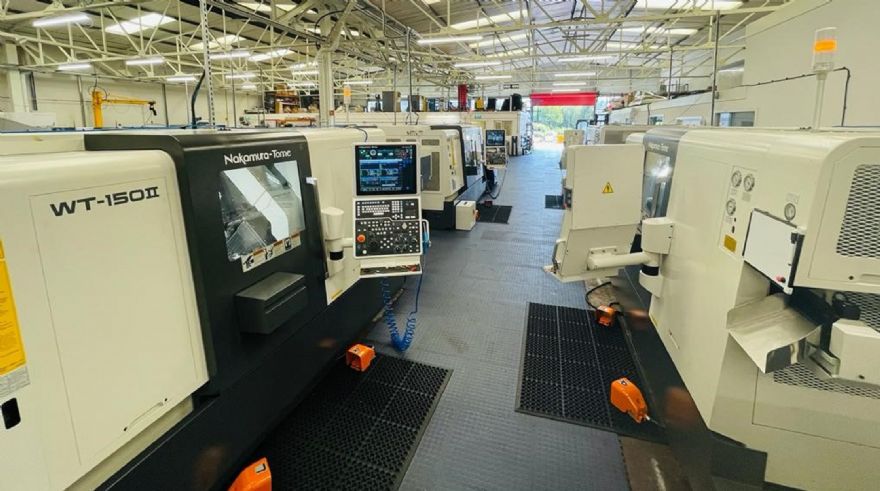
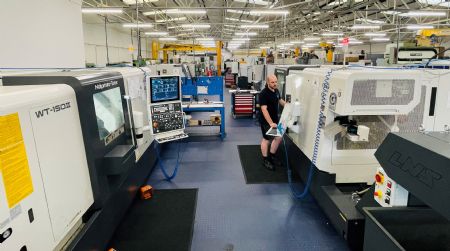
Quest Precision Engineering Ltd is on a trajectory of continuous growth to meet demand from its growing customer base in the oil and gas, electronics, automotive and aerospace sectors. The Scottish manufacturer initially acquired two Nakamura-Tome WT150II turning centres during the Covid-19 pandemic and has just added two more to the line-up at its 20,000ft
2 facility just outside Dundee.
All supplied by the
Engineering Technology Group’s (ETG) Scottish distribution partner Forfar-based
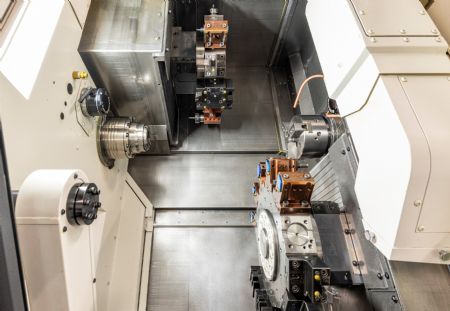
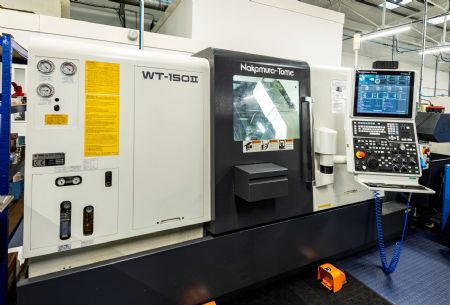
RAM Engineering and Tooling Ltd, the multi-tasking machine tools have future-proofed the ISO9001:2015-certified company which can machine everything from simple to the most complex components. The desire to machine complex parts from challenging materials in‘one hit’ led Quest install the first twin-turret WT150II Nakamura-Tome turning centre in December 2019. The impact of this machine resulted in a second machine being installed four months later and then two more at the end of July.
Before Quest installed its first Nakamura-Tome WT150II, it was machining autonomous valves for the oil and gas industry in five operations on four machine tools. The production of the complex 2in diameter Inconel 718 valves that control the flow of oil from wells was time-consuming and not cost-effective enough to compete with an existing Chinese supplier. To win more of the business from the overseas supplier, Quest needed to increase productivity and reduce costs.
Gordon Deuchars, Quest Precision’s managing director, said: “There are 25-30 different valves in the family of parts we manufacture and for us to win more business, we had to increase throughput and reduce costs to be cost-competitive with China. Ross Milne from RAM Engineering and Tooling discussed the merits of a Nakamura turnkey solution for the valves and the decision was made. It has been a revelation — the first two machines made a huge impact and brought us significantly more business. To support the subsequent growth and carry out yet more R&D work, we invested in the next two machines.”
Streamlining productionDepending upon the valve variant, the majority of valves were processed in 2-4 hours on four machine tools with an additional 25% set-up time across the numerous machines. Running everything from prototypes right through to production runs of 1,000-off, producing such volumes with the existing machine tools was unfeasible. The first twin-turret twin-spindle Nakamura-Tome WT150II immediately alleviated the situation, the second machine solved it and machines three and four are helping the company cope with an influx of new orders.
One-hit machining on the WT150II initially reduced cycle times by 50% to 1.5hr while freeing capacity and labour requirements throughout the shopfloor. Mr Deuchars continued: “The WT150II made such a difference to our production and set ups that we ordered a second machine within weeks. Instead of using multiple machines and up to five staff on the valves, we have one operator running the two Nakamuras.
“With one staff member running the machines on days and another on nights, the first two WT150II machines increased our productivity by 500%, making us cost-competitive with China. They also reduced our tooling costs considerably due to the machine set-up and rigidity. The latest two machines have immediately mirrored the success of the first two.”
The result of investing in the first two Nakamura machines significantly increased business from this particular offshore customer — and this is why two more WT150II machines have followed. As Mr Deuchers recalled: “The challenge this offshore customer had with supply from China was proximity, which made any R&D work, amendments or part inspection an issue. They can now easily visit our facility to discuss projects, look at our production methods and equipment and investigate opportunities to enhance and develop their product lines, all with a local supplier.”
“We started production on what they called the Mach 1, 2 and 3 valve designs. Now, we are fully integrated into the customers' R&D infrastructure, and we are working closely with them on the development of the Mach 4 valve. Since investing in the Nakamura machines, we have won much more business from this customer and the Nakamura’s are 95% dedicated to producing and undertaking R&D work on the Inconel valves.”
Looking specifically at the latest two WT150II machines, Mr Deuchers explained: “The latest machines have upgraded software, which has since been loaded onto the previous two machines. The software incorporates tool monitoring and tool wear notifications to ensure we maintain optimal cutting conditions and have no tooling failures. Additionally, the software has a new optimisation feature. With the touch of a button, it will review a programme and automatically make incremental improvements to tool path movements and reduce turret movements for tool changes. This has instantly shaved more than 30sec from some programmes.”
Mr Deuchers concluded: “The first two WT150II machines improved and streamlined productivity, reduced costs and enabled us to better allocate our staff, freeing up more than 15% of capacity from the rest of our facility. Evidently, the result of the initial investment won us a lot more work and this justified the purchase of the second two WT150II machines.
“Our next step will be to install the Amorphous Core Transformers (ACT) from ETG on the two newest Nakamuras. This will reduce our power consumption by more than 15%. Once installed, we can compare the financial and environmental benefits of the latest machines with their predecessors and we are committed to improving our carbon footprint and environmental credentials while running our business as efficiently as possible.”