 LEWA
, part of
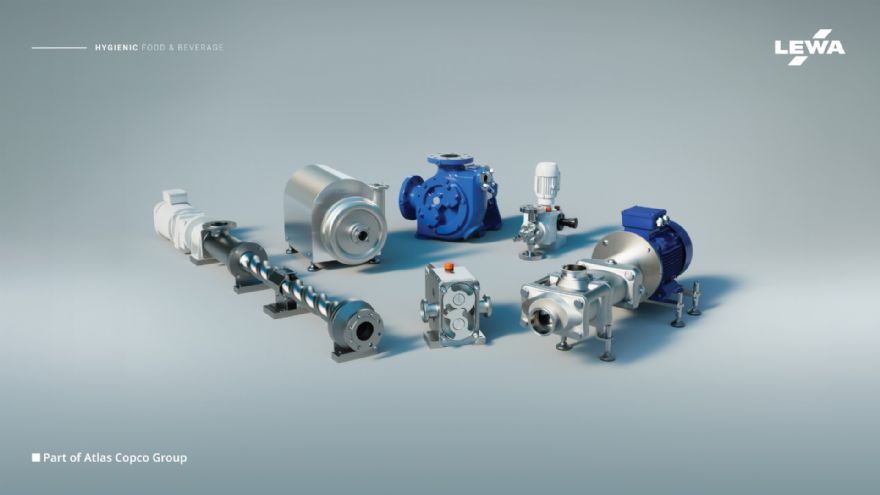
Atlas Copco Group Industrial Flow division, brings together a portfolio of hygienic industrial flow technologies designed to help manufacturers in the food and beverage industry maximise production efficiency while maintaining product integrity. This initiative integrates a full range of hygienic industrial flow technologies - including lobe, centrifugal, reciprocating diaphragm and plunger, progressing cavity, and twin-screw pumps, as well as customised metering and mixing systems - into a one-stop shop. The offer provides producers with a comprehensive portfolio of pumps, systems, and technical expertise tailored to meet the demanding operational requirements of modern food and beverage production.
Manufacturers face growing pressure to maintain strict hygiene standards, ensure consistent product quality, and optimise operational efficiency. The unified portfolio addresses these challenges by delivering advanced industrial flow technologies engineered for reliable and hygienic processing environments.
Ingo Landwehr, business line manager food and beverage, said: “Our focus is on helping producers achieve high uptime and operational reliability in food and beverage production, while safeguarding the integrity of their products. By bringing together our own technologies and decades of expertise across these solutions into one consolidated offering, partners, customers, and end users benefit from a single trusted source for hygienic, reliable, and energy-efficient industrial flow solutions, backed by dedicated experts.”
These solutions are engineered to meet stringent industry standards, ensuring safe and hygienic processing across applications from ingredient handling to finished product transfer. These technologies support production processes across a broad range of subsegments, including dairy, fruits and vegetables, beverages, prepared foods, pasta, cereals, meat, seafood, sugar, confectionery, bakery products, starch and proteins, or liquid foods, among others. The integrated food and beverage portfolio combines specialized pump technologies for diverse modern processing needs.
LEWA provides advanced diaphragm metering and process pumps (LEWA ecoflow™, LEWA ecodos™, LEWA triplex™), as well as customised mixing and metering systems, for precise, safe, and reproducible dosing of critical ingredients. Pomac™ lobe pumps gently handle shear-sensitive, high-viscosity products, while Pomac™ centrifugal pumps ensure efficient, cleanable transfer and consistent quality.
Wangen™ twin screw pumps handle a wide range of media with low wear and high uptime, and Wangen™ progressing cavity pumps enable hygienic conveying and dosing across varying viscosities, including solids. Complementing the portfolio, Varisco™ internal gear pumps provide smooth and controlled transfer of products such as syrups, oils, and chocolate in industrial food processes.
Together, these technologies form a consolidated portfolio, providing end-to-end solutions to enhance operational efficiency, maintain product integrity, and support the entire production chain, from ingredient intake and formulation to conveying, processing, and cleaning with Clean-in-Place (CIP) and Sterilise-in-Place (SIP) compatibility.
All these technologies are part of the Atlas Copco Group, with dedicated competence centres in the Netherlands, Germany, China and Italy. Supported by more than 17 customer centres worldwide, ensuring a strong global footprint with an established local presence in key markets, Atlas Copco Group serves the food and beverage industry with a unique and consolidated portfolio.
Beyond hygiene and product protection, these technologies are designed to support production reliability and operational efficiency. Energy-efficient pump designs and optimised system integration help manufacturers reduce operational costs while supporting energy efficiency and maintaining high levels of uptime.
LEWA complements its technology portfolio with dedicated expert support across the entire lifecycle of food production pumps and systems. Services include application engineering, system design, commissioning, maintenance, and training. With global expertise and local service capabilities, the brand supports producers in addressing complex processing challenges and maintaining reliable production performance.
Stefan Glasmeyer, VP sales and marketing, said: “Food and beverage producers need partners who understand their processes and the critical role of hygienic flow technology. We bring together the technologies and expertise needed to support manufacturers and system integrators at every step of their production.”