The
Horn Cutting Tools stand at
Southern Manufacturing & Electronics 2027 (A205) will centre on a lineup of its latest high-performance indexable-insert tooling innovations, led by the S234 parting-off products and the S66T grooving systems, alongside the Mini and Supermini tool ranges.
All inserts feature chip breaker geometry pressed accurately, repeatably and economically into each green blank before it is sintered. It saves the expense of having to laser-cut or grind the geometry into the insert after it has been hardened. Until now, this has been the industry norm when manufacturing miniature inserts due to the difficulty in pressing small chip breaker forms without them losing precision when heated at up to 1,500°C in a furnace.
Indexable-insert tool for parting-offThe S234 system was developed by Horn especially for large parting depths. The double-edged system enables a maximum depth of cut of 33 mm for reliable, economical parting off. The combination of large grooving depths, rigid clamping, high-performance sintered EN chip breaking geometry and internal cooling makes the system attractive in terms of price and performance.
The inserts are available in cutting widths of 2mm or 3mm and the corner radii are 0.2mm and 0.3mm respectively. Depending on the material to be machined, they are available in AS65 and IG65 grades. Square shank holders in sizes 20mm x 20mm and 25mm x 25mm ensure stable clamping and they are equipped with internal coolant supply.
Six-edged radial grooving insertsWith the latest S66T grooving system, Horn has expanded its cutting tool portfolio in the area of six-edged indexable inserts, which offer a competitive price per cutting edge. Maximum grooving depth is 9.5mm, which is about 4mm more than is possible with the sister system, 64T. Cutting width is either 2.5 mm or 3mm and the corner radius is 0.2mm.
Depending on the application, to ensure reliable chip management Horn offers the neutral grooving inserts with a choice of two chip breaker geometries, 1A for groove turning operations only, or DL for longitudinal turning as well as grooving. There is a further version without geometry for maximum edge strength. The IG65 carbide grade is used for machining stainless steels and difficult-to-cut materials, while for general steels Horn recommends the EG55 carbide grade. For the former operation, the inserts are available with a corner radius of 0.4mm.
 Pic: Horn inserts for the S66T grooving system
The variants with chip breaker geometry ensure excellent surface quality on the groove flanks and the straight main cutting edge produces a cleanly finished base. They can be clamped in square shanks, with internal coolant delivery to either the left- or right-hand side.
Sintered inserts for the Mini systemHorn has also developed sintered chip breaker inserts for its Mini tool system. Featured on the stand will be Mini types 108, 111 and 114. Their sintered I-Geometry is particularly aimed at machining materials with poor chip formation properties. It is suitable for copy turning, longitudinal turning, back turning and facing. Especially with shallow depths of cut in steel and stainless steels, the tool system with this geometry demonstrates effective chip control. It leads to higher process stability and longer tool life.
When developing the I-geometry, Horn took into account the machining of lead-free materials. As these will pose a challenge in the future due to their inferior chip formation, the tool manufacturer offers inserts with small corner radii starting from 0.05 mm for small lateral infeeds.
The face-mounted, screw-on, Mini-type inserts are among Horn's core products. The tool system is suitable for turning and milling applications. The precision tools have proven particularly effective for internal turning and grooving. With the low-vibration, solid carbide tool holders, the inserts produce good surface finishes even with long overhangs and ensure high process reliability.
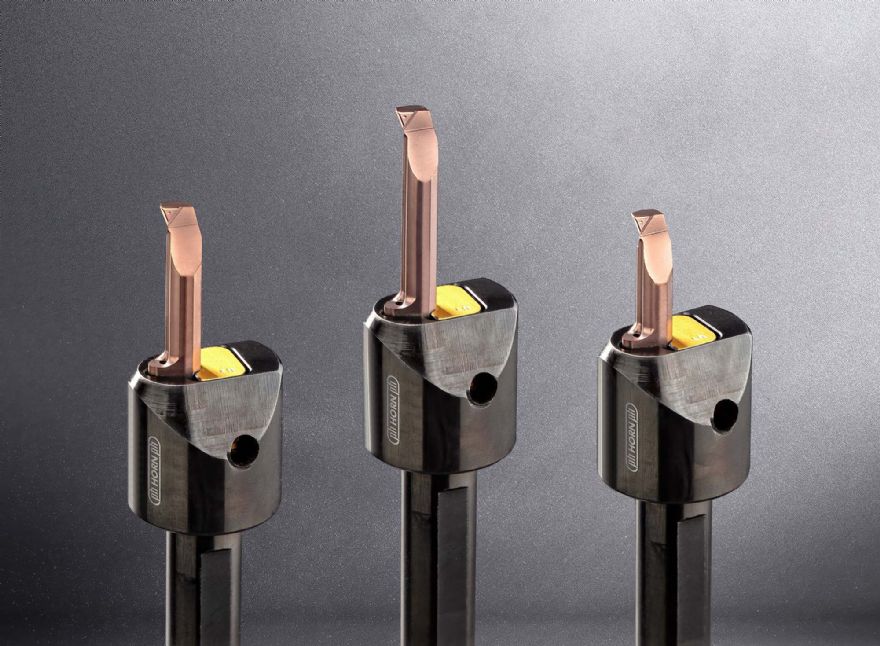
Economical boring toolsHorn’s Supermini universal boring system has undergone numerous development stages over the years and has solved problems in a variety of turning applications. Another milestone has been announced for the Supermini type 105, namely a lower cost version of the carbide inserts with sintered chip breaking geometry, called GM (geometry moulded), with a price similar to that of the standard insert without a chip breaker.
 Pic: Face grooving to a depth of up to 10mm is possible with Horn's Mini system with I-Geometry
The inserts assist internal machining of small diameter holes, whether profile turning, internal grooving, threading, chamfering, face grooving or slot broaching. Horn developed teardrop shaped carbide blanks for the tool, enabling large, precise contact surfaces in the tool holder and resulting in greater rigidity of the overall system. Furthermore, the teardrop profile prevents the insert from twisting, which leads to consistent, precise positioning of the centre height of the tool. When using long tool overhangs, it reduces deflection and minimises vibration during turning.
Horn offers the inserts as standard in three lengths (15.0mm, 20.0mm and 25.0mm) and in carbide grades TH35 and IG35. The tool is suitable for use from a bore diameter of 6mm. The cutting edge geometry extends far into the 0.2mm corner radius of the insert, ensuring good chip control even with small infeed settings. Different material groups may be processed and the geometry is suitable for internal, face, copy and back turning.
The new insert is compatible with numerous 105 tool holders, including round shank, square shank, interface and adjustable types. There are four different solutions for clamping the inserts: a classic ball pressure screw, a face clamping element, a lifting element, and for confined spaces, a compact system with clamping via a union nut. In addition, Horn's applications department solves users' specific machining problems with customised solutions.
Top pic: Horn Supermini boring tools