UK packaging machine specialist
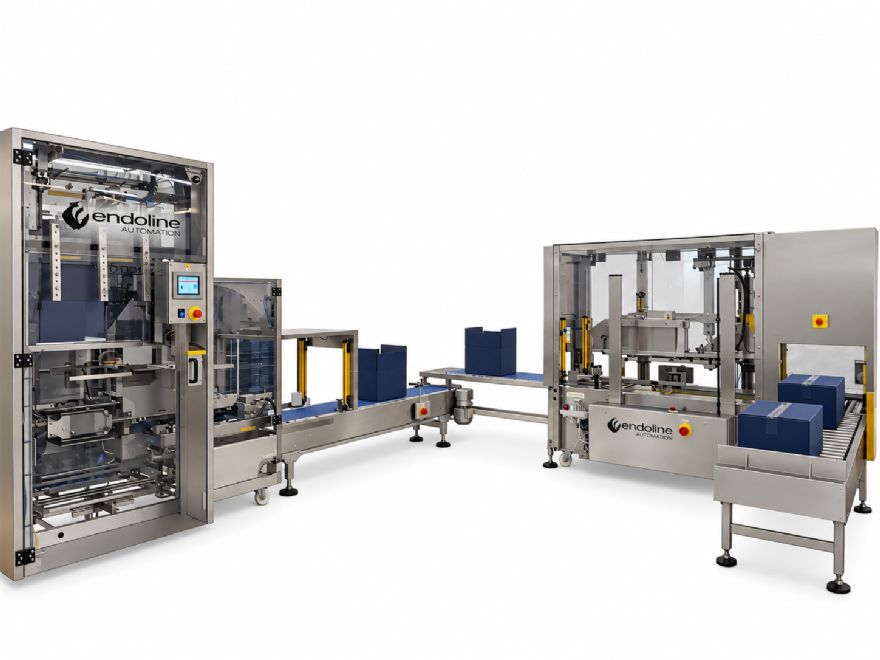
Endoline has won a landmark export project installing four bespoke case erecting and sealing systems at a major biotech facility in Ireland. This high-spec customisation project marks Endoline’s global debut in automating the assembly of expensive plastic cases in a sterile, cleanroom packaging environment.
Four identical IP65-rated 221 case erectors and 702 case sealers were specially adapted by Endoline to assemble and seal hygienic, high-value biotech plastic shipping cases. Unlike cardboard, which gives off dust that can contaminate a sterile environment, these plastic cases provide a completely dust-free and hygienic solution. They also feature special blue filters that protect pharmaceutical vials by limiting exposure to light, moisture and fluctuations in temperature.
Given that each plastic case costs more than fifty times the price of a cardboard alternative, the Endoline team re-engineered each machine to ensure absolute reliability. James Ramsay, Endoline’s export manager, said: “Plastic behaves very differently to traditional cardboard. To automate the case erection and assembly process the Endoline engineering team had to completely rethink and modify the hopper feed and overlap closing flap sequence.” This involved modifying pneumatic safety controls and refining gentle handling mechanisms to ensure that delicate vials are protected from vibration or damage during international transportation.
Health and safety protocols within cleanroom environments are subject to far stricter regulations than standard manufacturing settings. These controls, for example, mean that operators are not permitted to intervene or open a machine to resolve minor production issues. The integrity of the sterile environment must be preserved at all times. Mr Ramsay added: “For high-value biotech products, automated systems are not just important for efficiency. They are a necessity to maintain the stringent environmental controls required in sterile pharmaceutical manufacturing. Any unauthorised interaction could potentially cause a contamination risk and significant production downtime.”
The US-based biotech customer made it clear from the outset that one of the key reasons for selecting Endoline for this project was its status as a UK manufacturer. To guarantee 100% operational reliability, Endoline undertook significant redesigns of several critical machine elements. Mr Ramsay said: “Our willingness to customise and geographic proximity really was a deciding factor in this case.” This flexibility played a key role in securing the contract and delivering on the customer’s exacting standards.
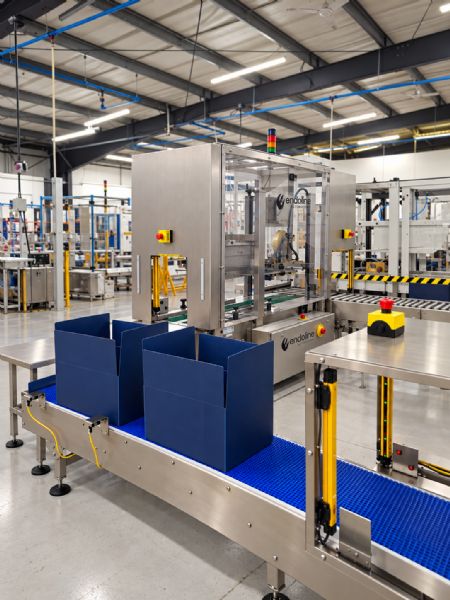
Although the system is designed to handle only one case size, the flap folding sequence had to be configured to accommodate the unique O204 configuration. For the 221 case erector, this involved developing bespoke rocket bars and forming arrangements to ensure the overlapping and non-standard flap lengths closed smoothly every time, without any risk of snagging. All four systems are constructed from high-grade stainless steel using IP65-rated components, ensuring full compatibility with intensive washdown procedures. Meeting these cleanroom specifications was essential for the customer’s internal validation processes, specifically their Installation Qualification (IQ) and Operational Qualification (OQ).
To support the hygienic touch-free ecosystem within the assembly cell, Endoline integrated several operator-centric innovations. For example, manual hopper latches were replaced with a pneumatic switch system to mitigate safety risks. This feature enables operators to reset the hopper via an automated button. Additionally, Endoline integrated a traffic light system. This instructs operators on when it is safe to interact with the machine to load new flat case blanks.
Further modifications were also made to the 702 top sealer. To protect delicate pharmaceutical vials, Endoline engineers adjusted the pressure on the top sealer’s folding arms. A pneumatic lift was also implemented, allowing cases to roll gently down the conveyor without incurring abrupt movements.
Each of the four systems is deliberately programmed to assemble, fill and seal no more than two cases per minute. On demand sensors were added to monitor conveyor levels and pause production automatically. This helps prevent an accumulation of vials and synchronises production with the rate at which operators load trays into the cases. Mr Ramsay emphasised: “Having a steady throughput is a calculated strategy. By prioritising gentle product handling and 100% reliability, compliance and safety are never compromised.”
The strategic proximity and commercial ties between the UK and Ireland provided the initial foundation for this biotech partnership. However, the technical success achieved in Dublin now serves as the primary lever for global expansion, claimed Mr Ramsay. He said: “By proving that 100% reliability is achievable with high-cost, difficult materials in a cleanroom environment, Endoline has created a clear pathway to serve more customers, including cleanroom facilities. More than anything, this project confirms Endoline’s capability to transform niche, high-stakes challenges into repeatable, global manufacturing solutions.”
In the past three years, Endoline’s export business has grown by over 137%. Ireland is currently one of Endoline’s largest export markets. The success of this project also provides a strong reference point as the company targets further international growth, including expansion in the US through new distributor Hamrick and its presence at PACK EXPO International. This sustained international growth saw Endoline named Gold Winner – Exporter of the Year at the 2026 SME Bedfordshire Business Awards.